 Defining E-Mobility
Menu
Every controller is stress-tested and leak-tested before it ships.
Our plant in Mysuru builds the controller range on an interlinked line, under an ISO 9001:2015 certified quality system.
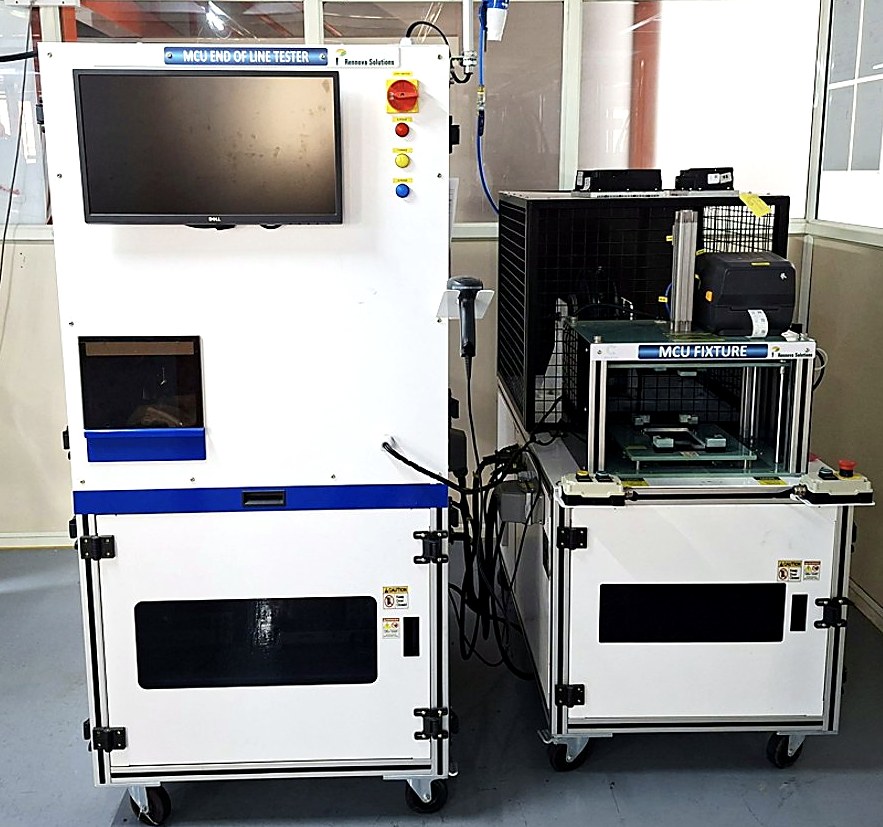
The line, station by station
-
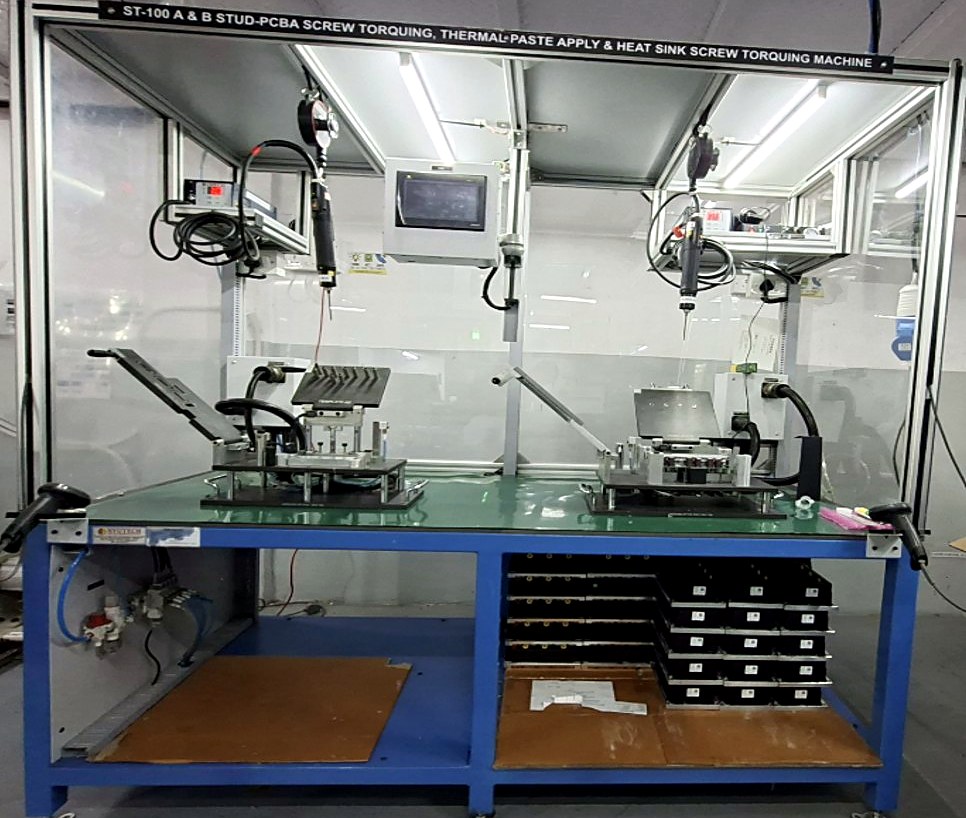
ST-100
Torquing and thermal paste
Studs and the PCB assembly are fixed to the bottom case with torque-controlled nut runners. Every torque is counted.
-
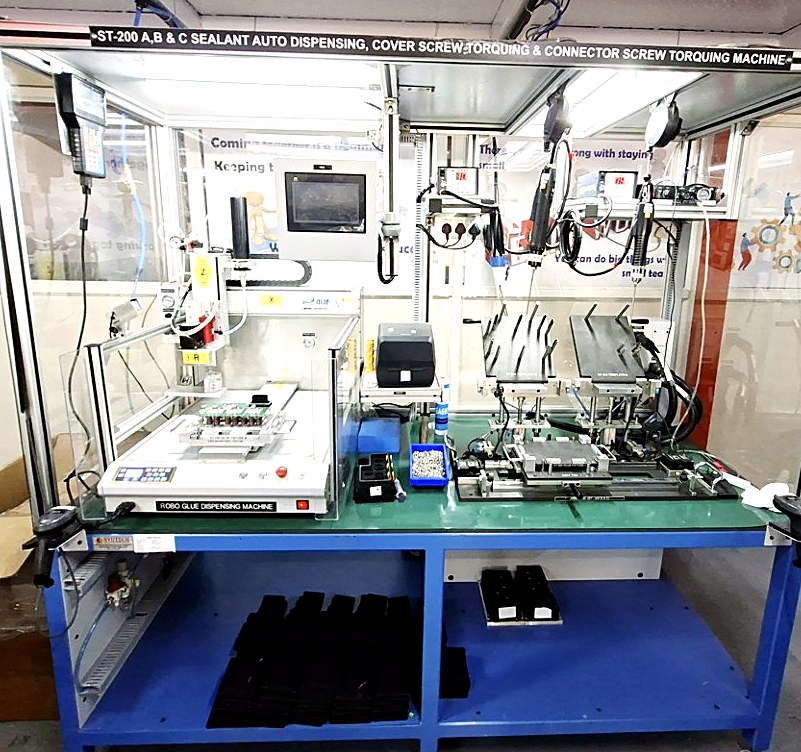
ST-200
Automated gluing and top case
Robotic gluing seals the case, then the top cover is torqued on.
-
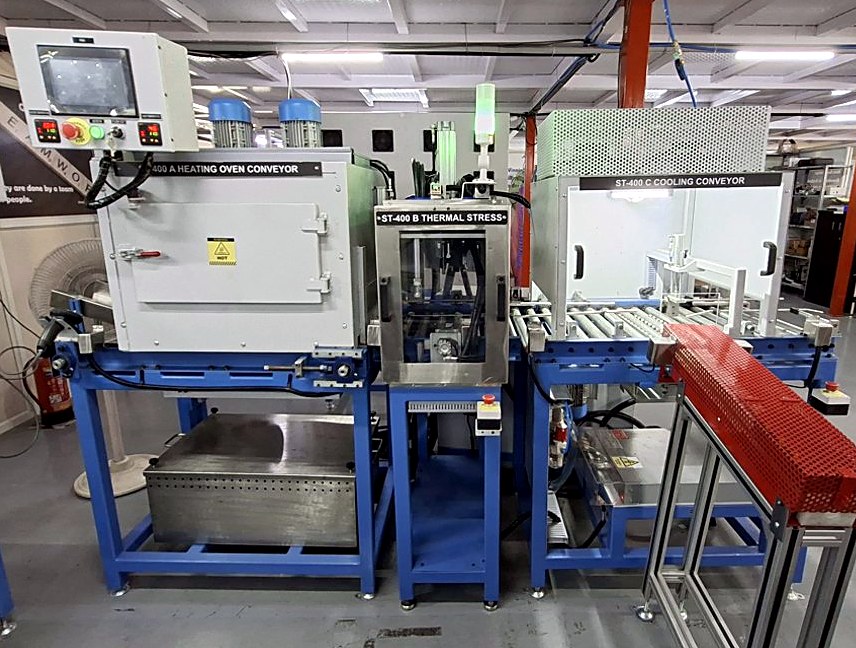
ST-400 / TEST
Thermal stress test
Each unit carries full load current until it reaches thermal cut-off, between a heating conveyor and a cooling conveyor. Units that fail are rejected automatically.
-
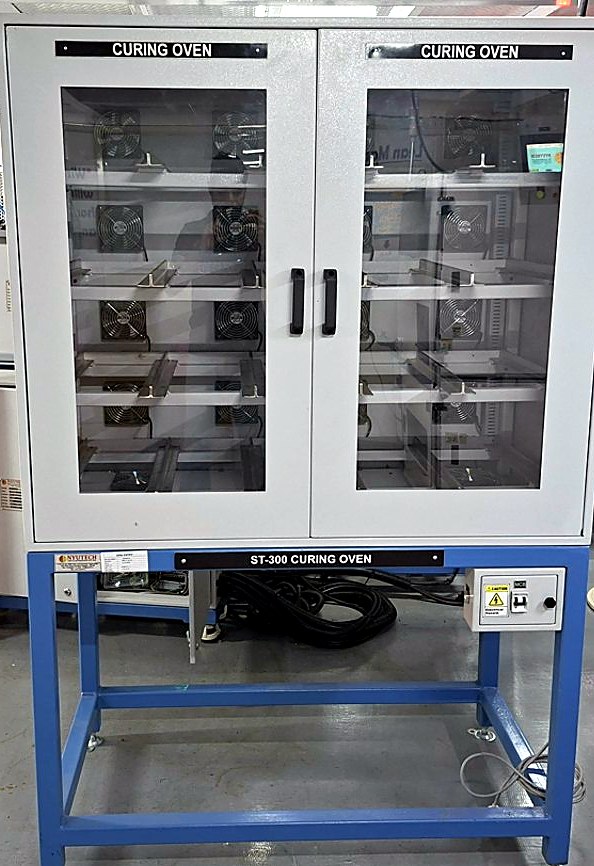
ST-300
Curing
The sealed unit cures in a curing chamber.
-
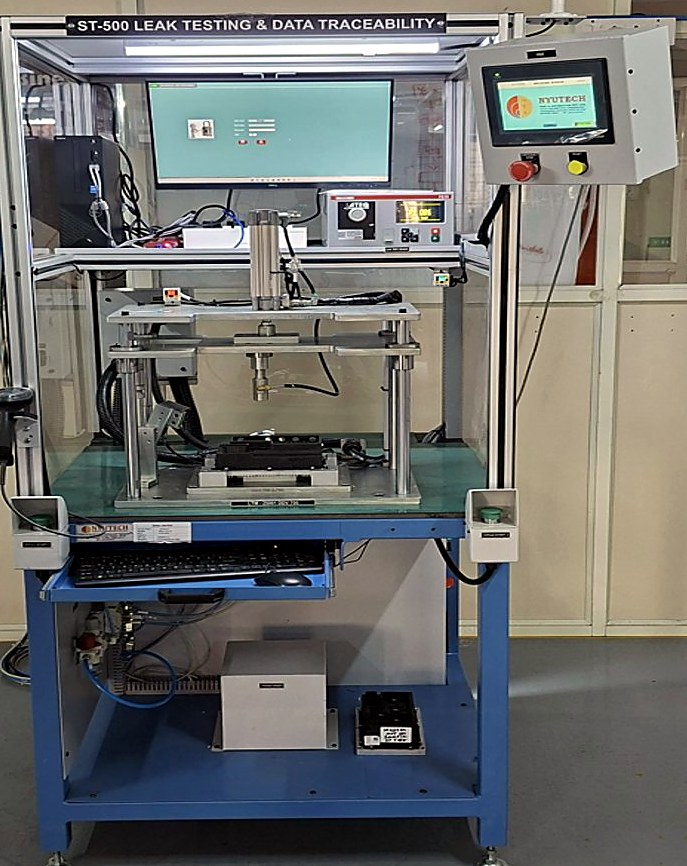
ST-500 / TEST
Leak test
A two-stage leak check on every unit for IP67, interlinked with curing time.
-
EOL / TEST
End-of-line test
Every parameter in the specification is tested before the unit is released.
Grommet and gasket assembly, bolt assembly with visual inspection, and a final inspection complete the build.
Error-proofing built into the line
Stations interlinked
Every station is linked through to end-of-line, so a unit cannot skip a step.
Full traceability
Data from each station is stored on a central server.
Locked parameters
Process parameters are password-protected, with user levels from operator to admin.
ESD-protected assembly
Assembly machines are ESD protected, with supervisory control for rework and repair.
ISO 9001:2015 certified.
- Sites covered
- Kochi and Mysuru
- Scope
- Manufacture of electric powertrain solutions for two- and three-wheelers: motor controllers, instrument clusters and motors
- Certifying body
- Magnitude Management Services Pvt. Ltd.
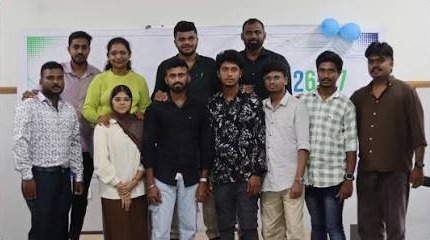
Our production team.
The team that assembles, tests and ships every C-Electric controller.
Want to see the line?
Plant visits and audits can be arranged for vehicle programmes.